Humidity Test Chamber About
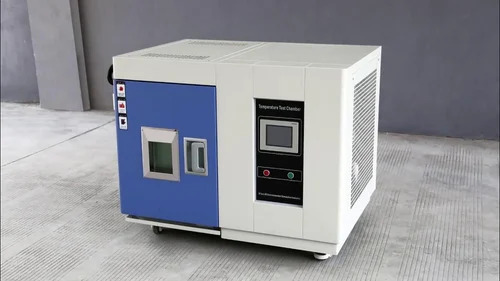
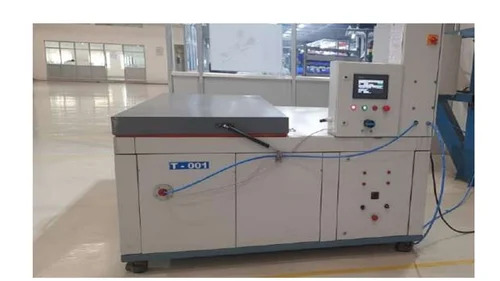
Explore the redoubtable Humidity Test Chamber with shelves, designed for blue-ribbon performance in both pharma and electronics industries. With a new, adjustable stainless steel interior and unparalleled corrosion resistance, this chamber ensures precise environmental testing. Advance purchase guarantees access to features such as a touch panel, capacitive humidity sensor, and LED internal lighting. The double sealed, tempered glass door, low noise operation, and caster wheels combine for seamless mobility. Crafted for reliability, this laboratory chamber is the definitive choice for uncompromised quality and performance in environmental simulation.
Commercial Applications & Key Advantages
The Humidity Test Chamber serves unrivaled versatility for commercial uses in pharmaceuticals, laboratories, quality control, and electronics manufacturing. Advantageous for its accuracy and blue-ribbon control, this equipment is trusted by leading researchers, product developers, and manufacturers. Its user-friendly digital display and automatic operation mode streamline workflows, enabling reliable tests and product validations. The chamber's robust build and tailored sizing ensure it remains a preferred solution among professionals seeking uncompromised environmental testing.
Availability, Packaging & Domestic Market
We maintain stock ready in India's main domestic mar, ensuring prompt delivery. Each Humidity Test Chamber is securely packaged to prevent transit damage and is handed over with proper documentation and installation support. With a reliable supply ability, we cater to laboratories, academia, and industries nationwide, offering customizable sizes and single phase power solutions to match precise user needs while maintaining strict adherence to safety and quality standards.
FAQ's of Humidity Test Chamber:
Q: How does the adjustable stainless steel shelving benefit laboratory operations?
A: Adjustable shelves offer flexibility to accommodate different sample sizes and test configurations, making the chamber suitable for diverse testing requirements in laboratories and industrial labs.
Q: What is the process for controlling humidity and temperature within the chamber?
A: The chamber uses a digital controller, capacitive humidity sensor, and a refrigerated cooling system to achieve and maintain targeted humidity (40%-95% RH) and temperature up to 60C, ensuring precision during testing.
Q: Where is this Humidity Test Chamber primarily used?
A: This chamber is widely used in pharmaceutical, electronics, and environmental testing laboratories for quality assessment, research, and product validation under specified humidity and temperature conditions.
Q: When can users expect the chamber to be supplied?
A: With stock ready and reliable supply chains, most orders in the domestic market can be fulfilled and handed over to customers rapidly, typically within standard business timelines depending on customization.
Q: What advantages does the double sealed tempered glass door offer?
A: The double sealed tempered glass door ensures excellent insulation, minimizes heat loss, and provides a clear view through the viewing window, all while maintaining a low noise level and secure environment for testing.
Q: How does overheat protection enhance safety during usage?
A: Overheat protection is integrated into the chamber to automatically activate safety mechanisms, thereby preventing potential damages or hazards during extended testing sessions and ensuring user safety at all times.




 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
 Send Inquiry

 Send Inquiry


